Everything You Need to Verify Before You Order
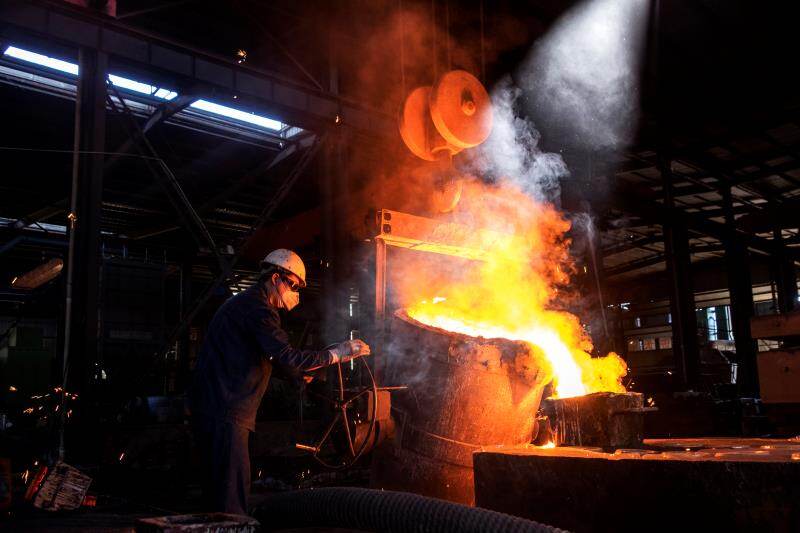
Melting, heat treatment, moulding, machining and inspection are all carried out in our own plant, with a record attached to every casting.
- 16,000 t
- 5–19,000 kg
- 7
Headquarters and Manufacturing Plant
Sichuan KINTES Technology Co., Ltd. manages engineering and sales from its headquarters; production and quality assurance are handled at its casting plant in Dechang.
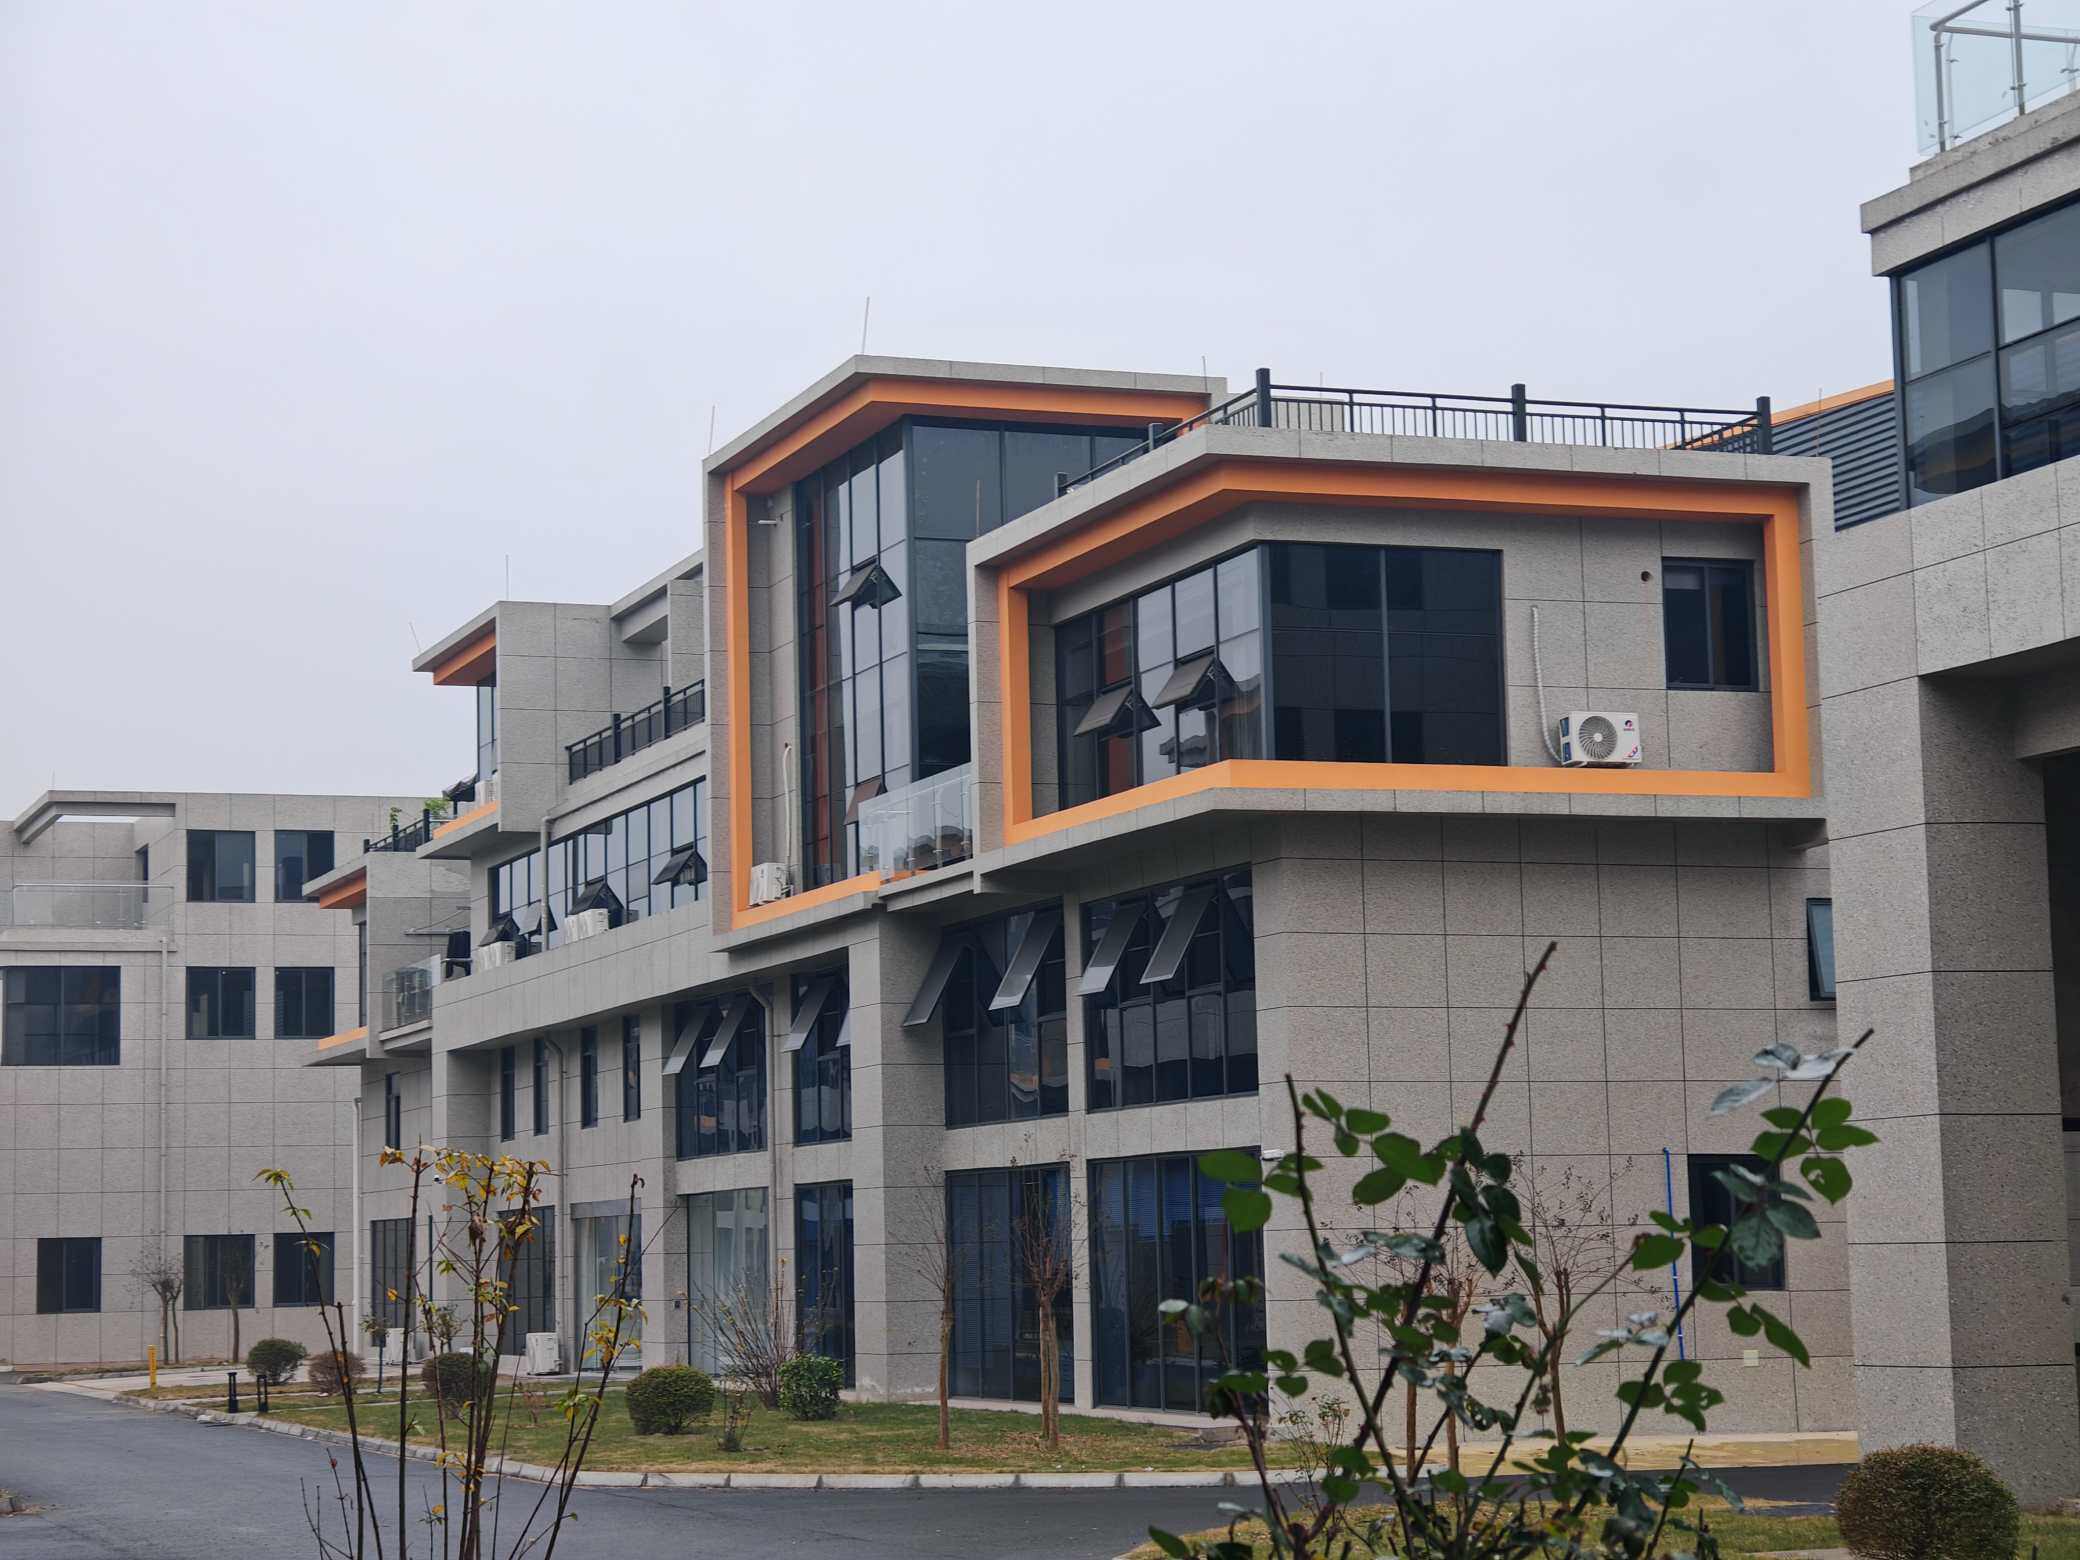
Sichuan KINTES Technology Co., Ltd.
Hi-Tech Zone, Chengdu, Sichuan, China
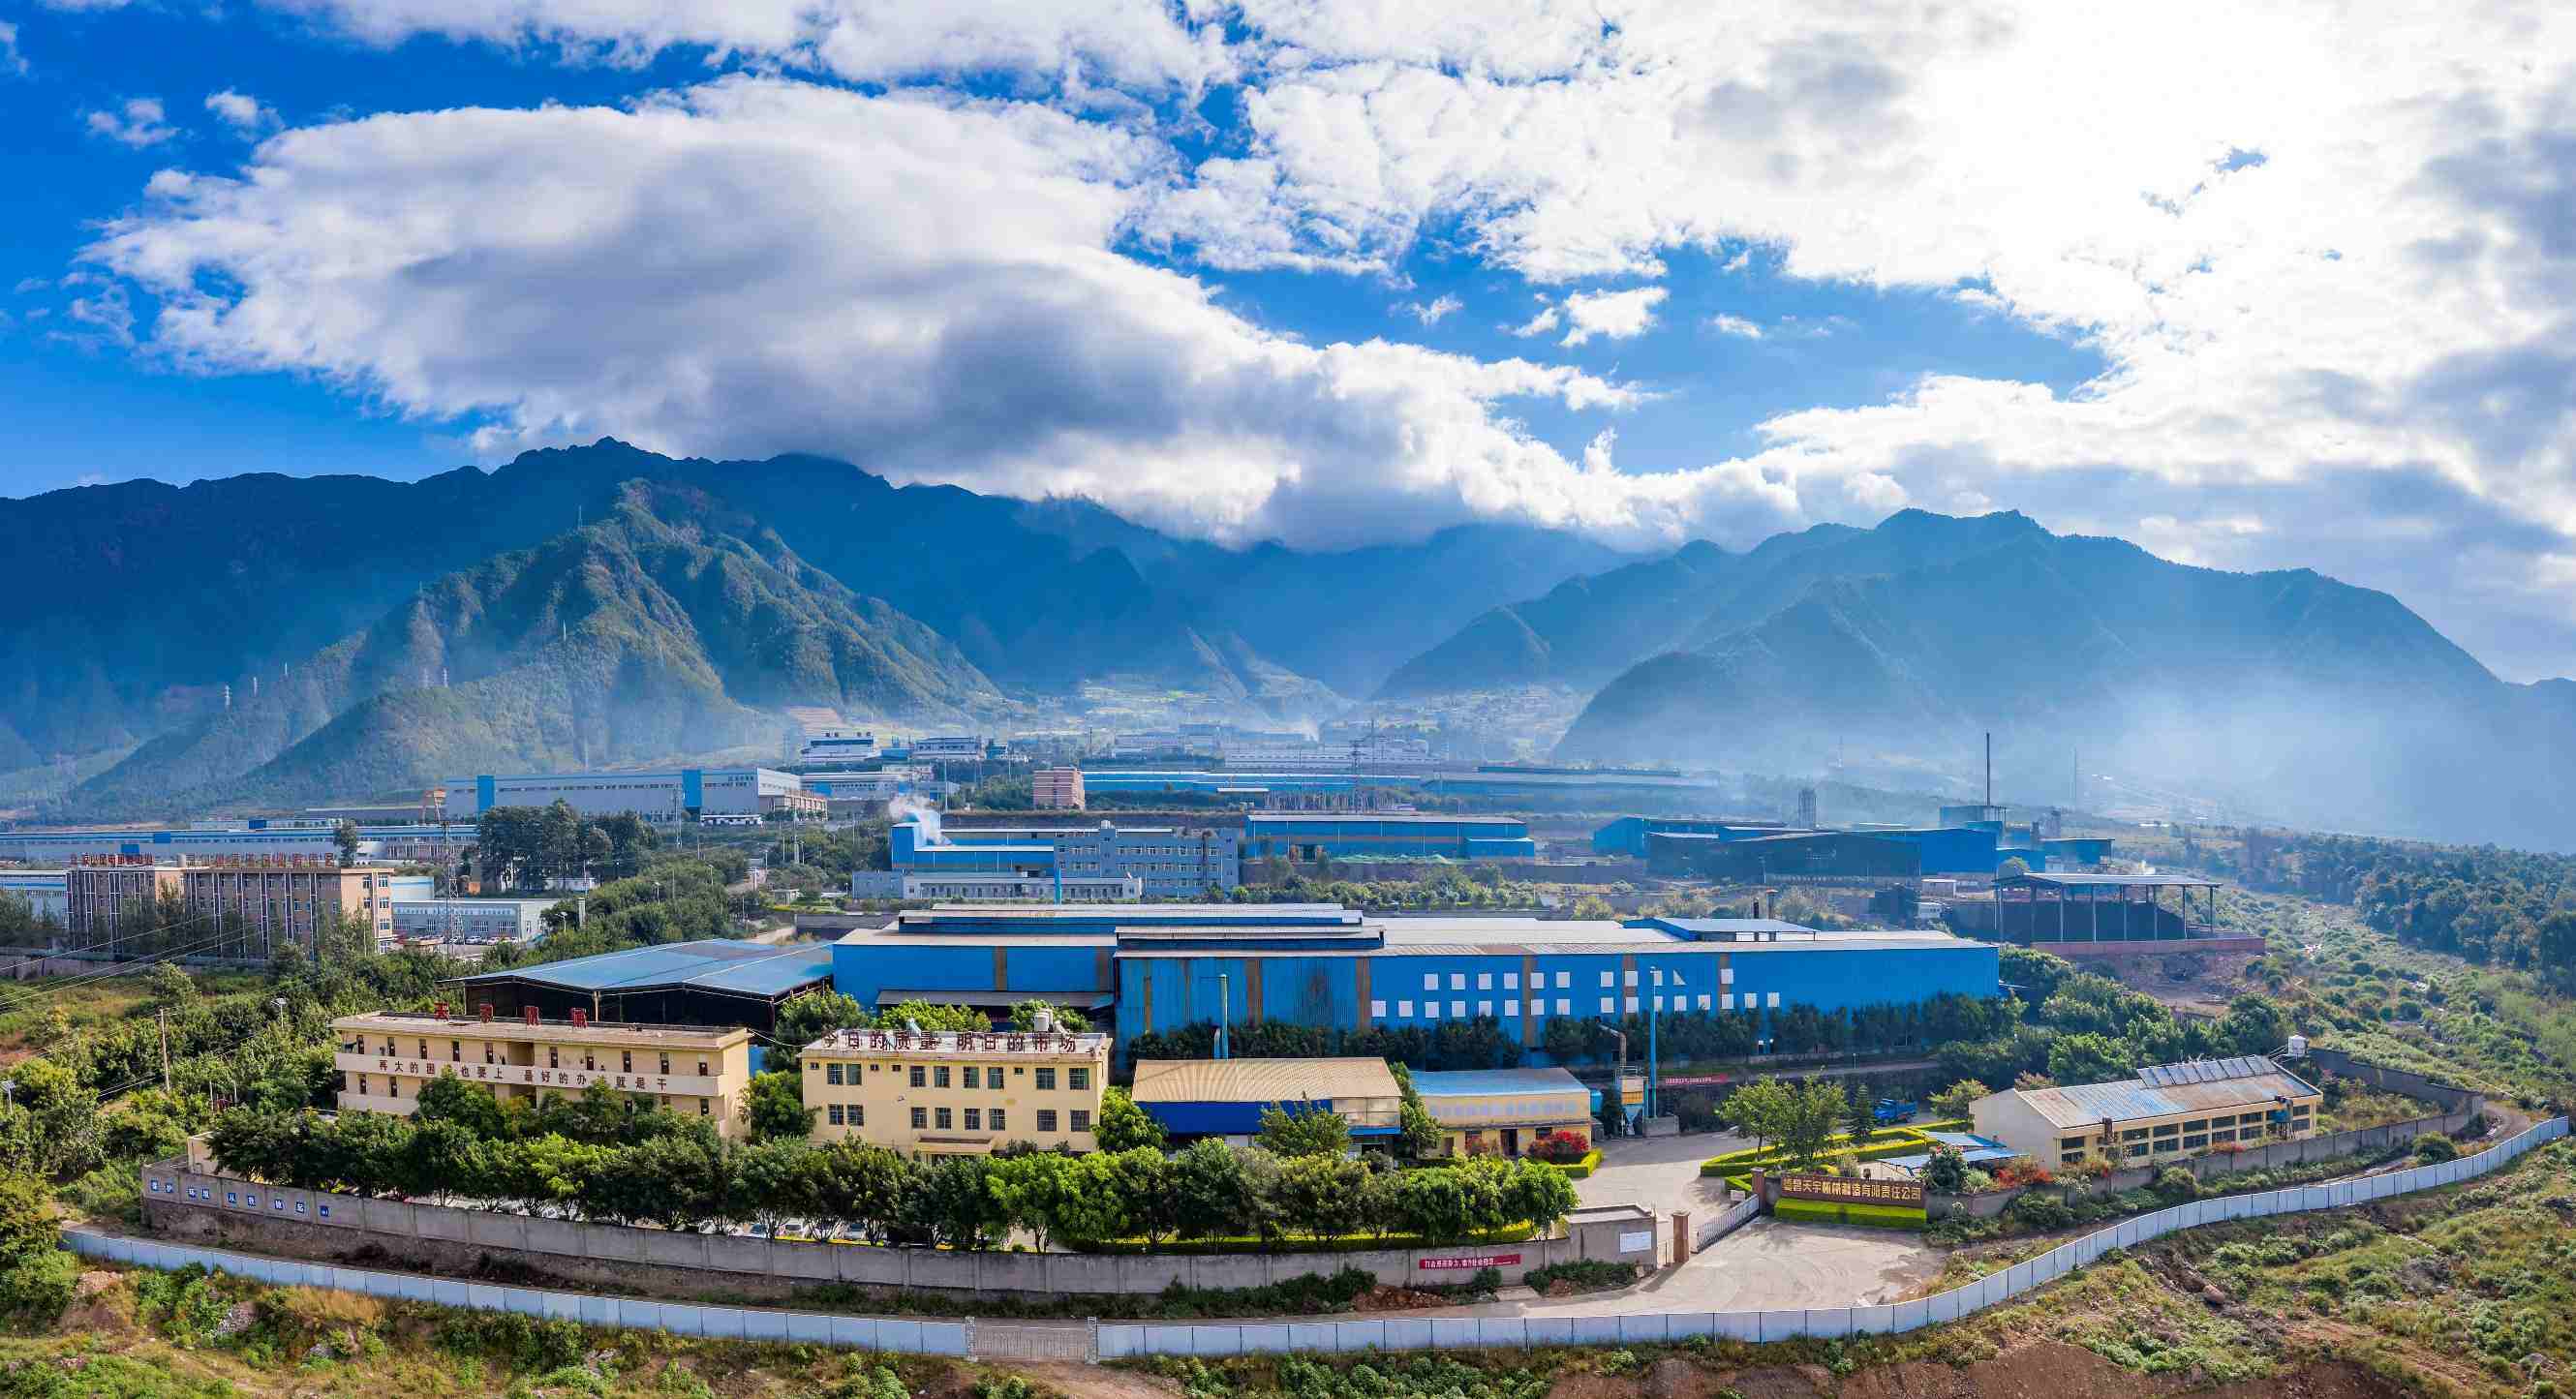
Dechang Xingyu Machinery Manufacturing Co., Ltd.
Dechang Industrial Park, Dechang County, Sichuan, China
From Melting to Machining
The equipment used to produce our wear parts, grouped by production stage.

Melting
- 1 × 1.5 t electric furnace
- 1 × 2 t electric furnace
- 2 × 5 t electric furnaces
- 1 × VOD furnace

Heat Treatment
- 7 × heat treatment furnaces
- Controlled heating and cooling cycles

Moulding
- 3 × moulding areas
- 3 × moulding lines
- 7 × sand mixers
- 2 × shot blasting machines

Machining & Lifting
- 15 × machining equipment sets
- Overhead cranes from 5 t to 50 t
- Large structural part machining
What We Cast and How Much
Six material families, three production lines, and a single-part weight range that covers everything from small wear inserts to heavy rotor and structural castings.
3,000
t / year
High manganese steel & high chrome iron
Cone liners, jaw plates, liners, blow bars and similar wear castings.
5,000
t / year
High strength martensitic cast steel
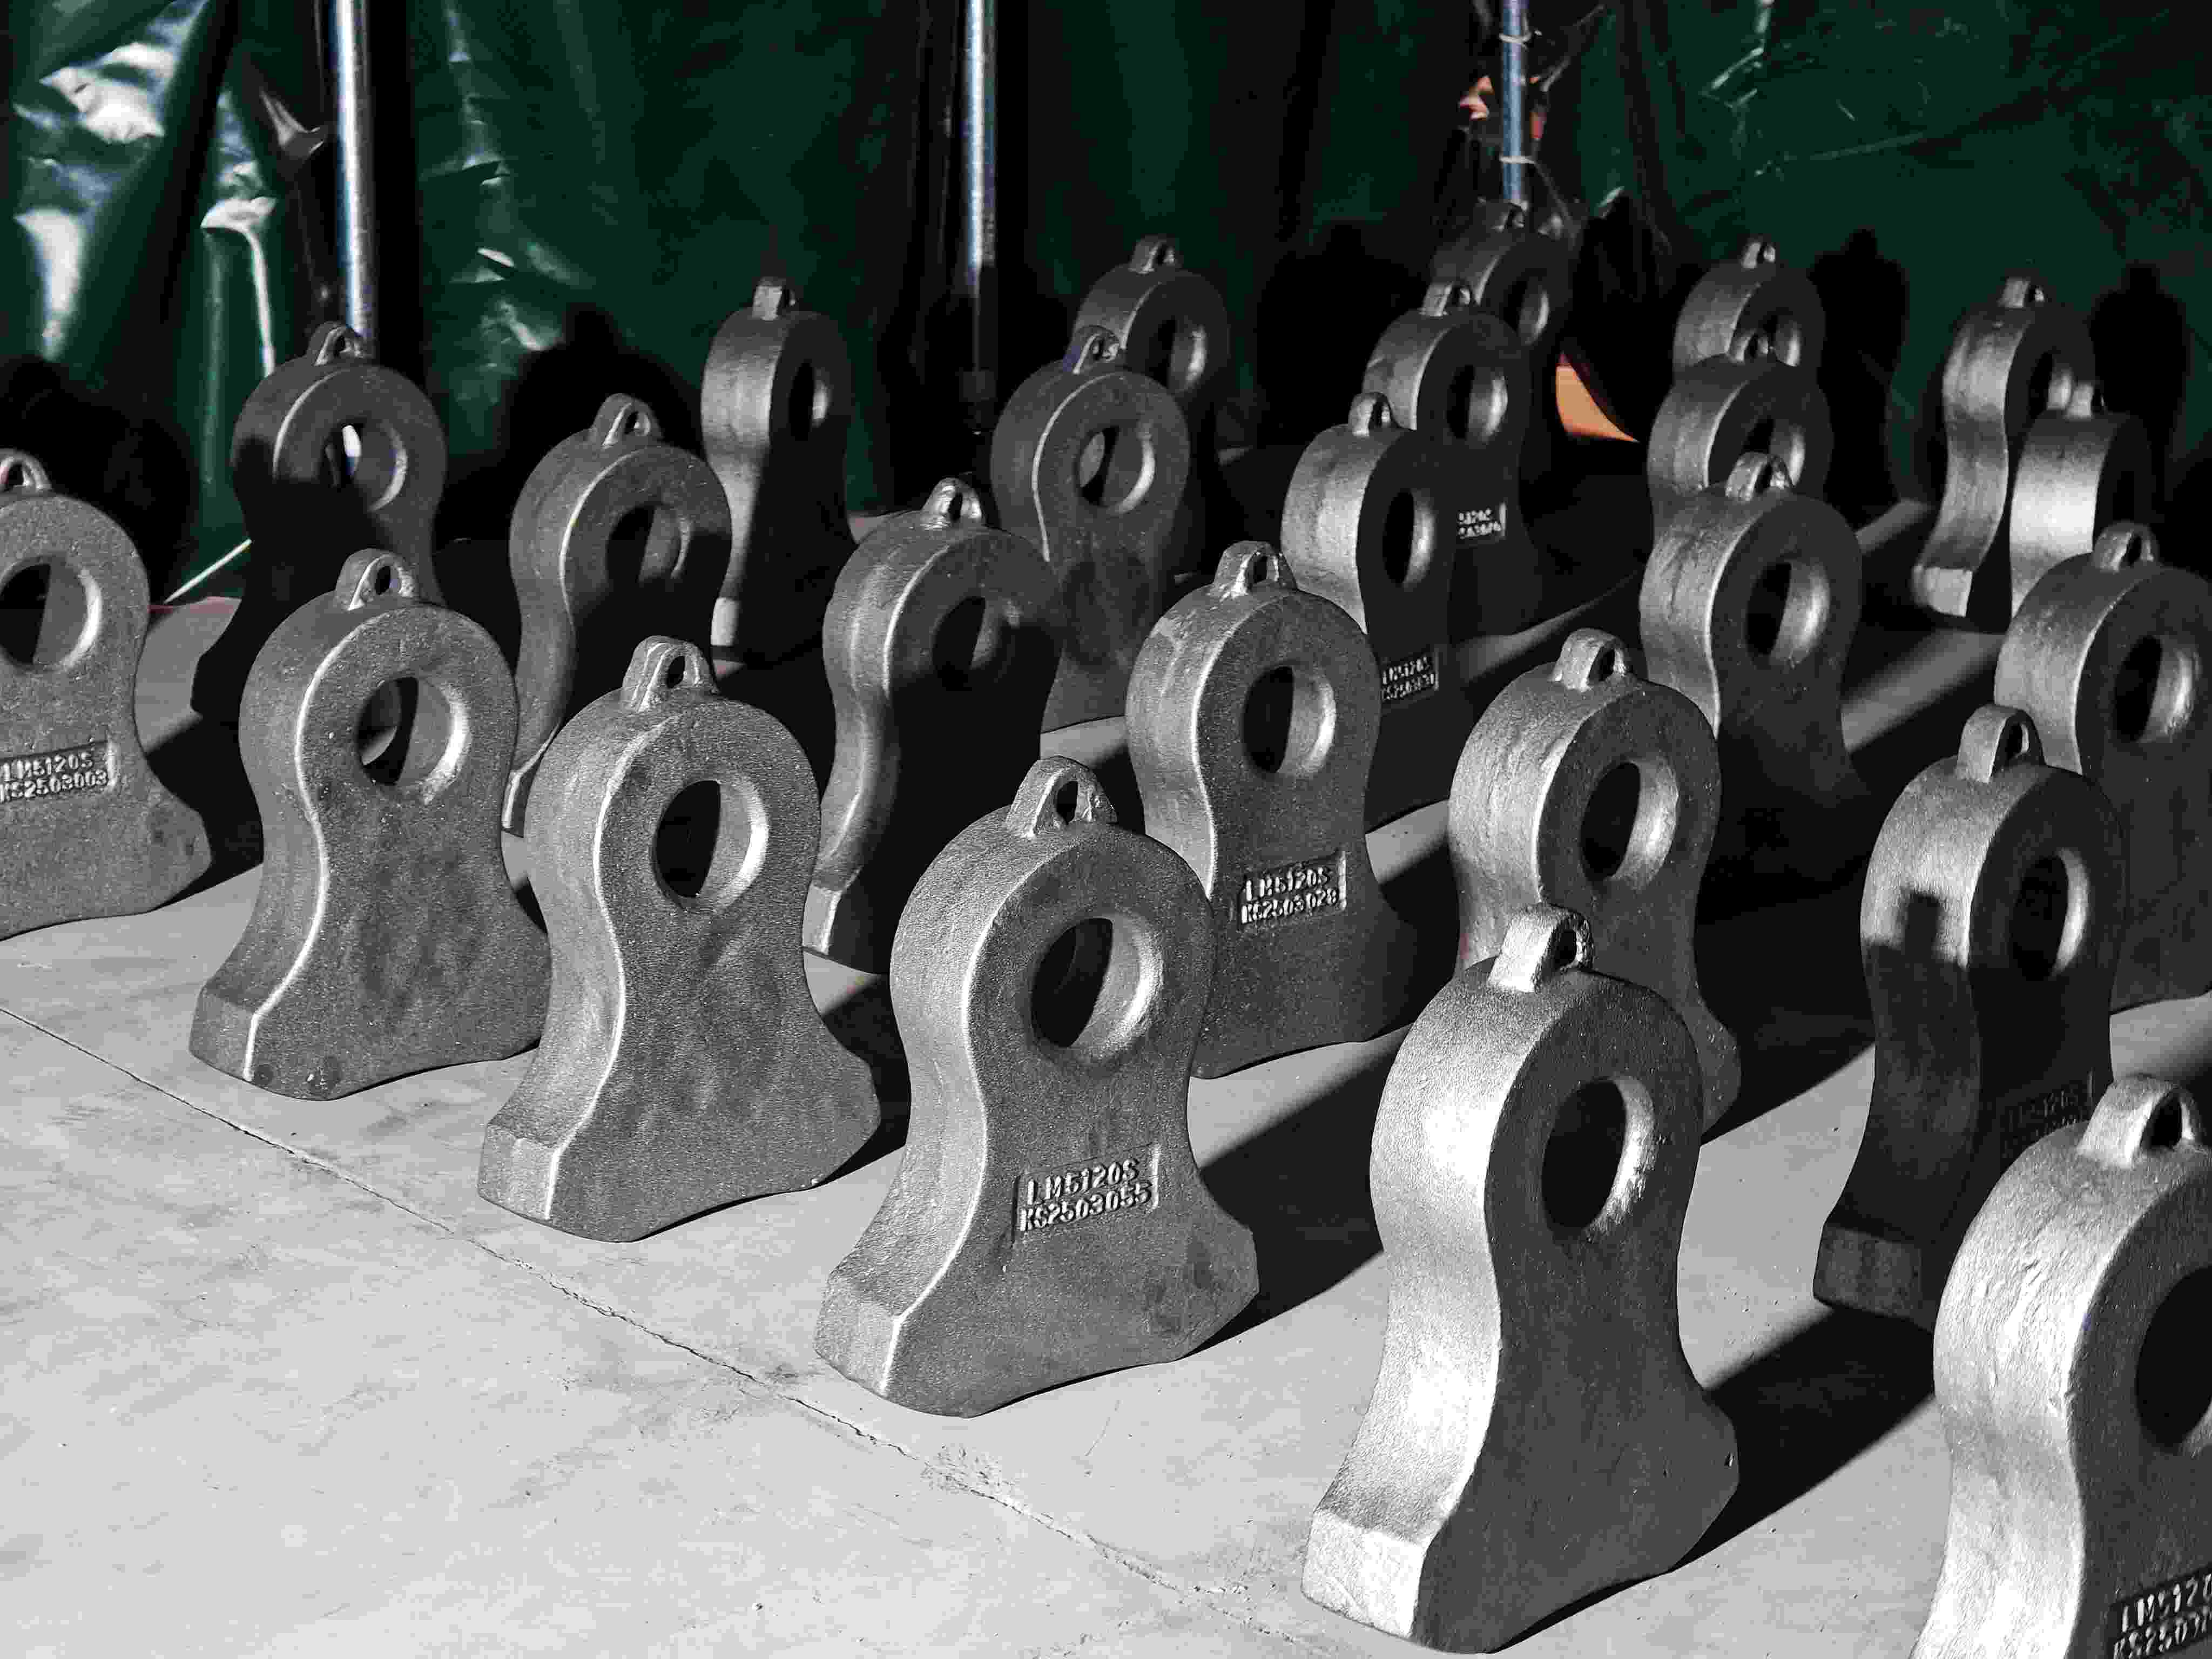
Hammers, grids, anvil , front wall castings, rotor caps, mill liners.
8,000
t / year
Carbon steel, chrome-moly steel & stainless
Structural parts, shafts, fabricated and machined assemblies.
5–19,000
kg
Single piece weight range
From small wear inserts up to heavy rotor and structural castings.
Materials we produce
Verification Before Batch Production
New products are first produced as trial parts. Parts that have not been produced for an extended period are re-verified by first-piece inspection. Batch production begins only after this verification.
Sample development trial
Every new product goes through a sample trial. Batch production starts only after the sample meets all inspection requirements.
First article inspection
For products not produced for a long period, the first piece is fully inspected and confirmed acceptable before the batch production.
Simulation before pouring
MAGMA casting simulation, introduced in 2017, verifies riser feeding and supports casting soundness before production starts.
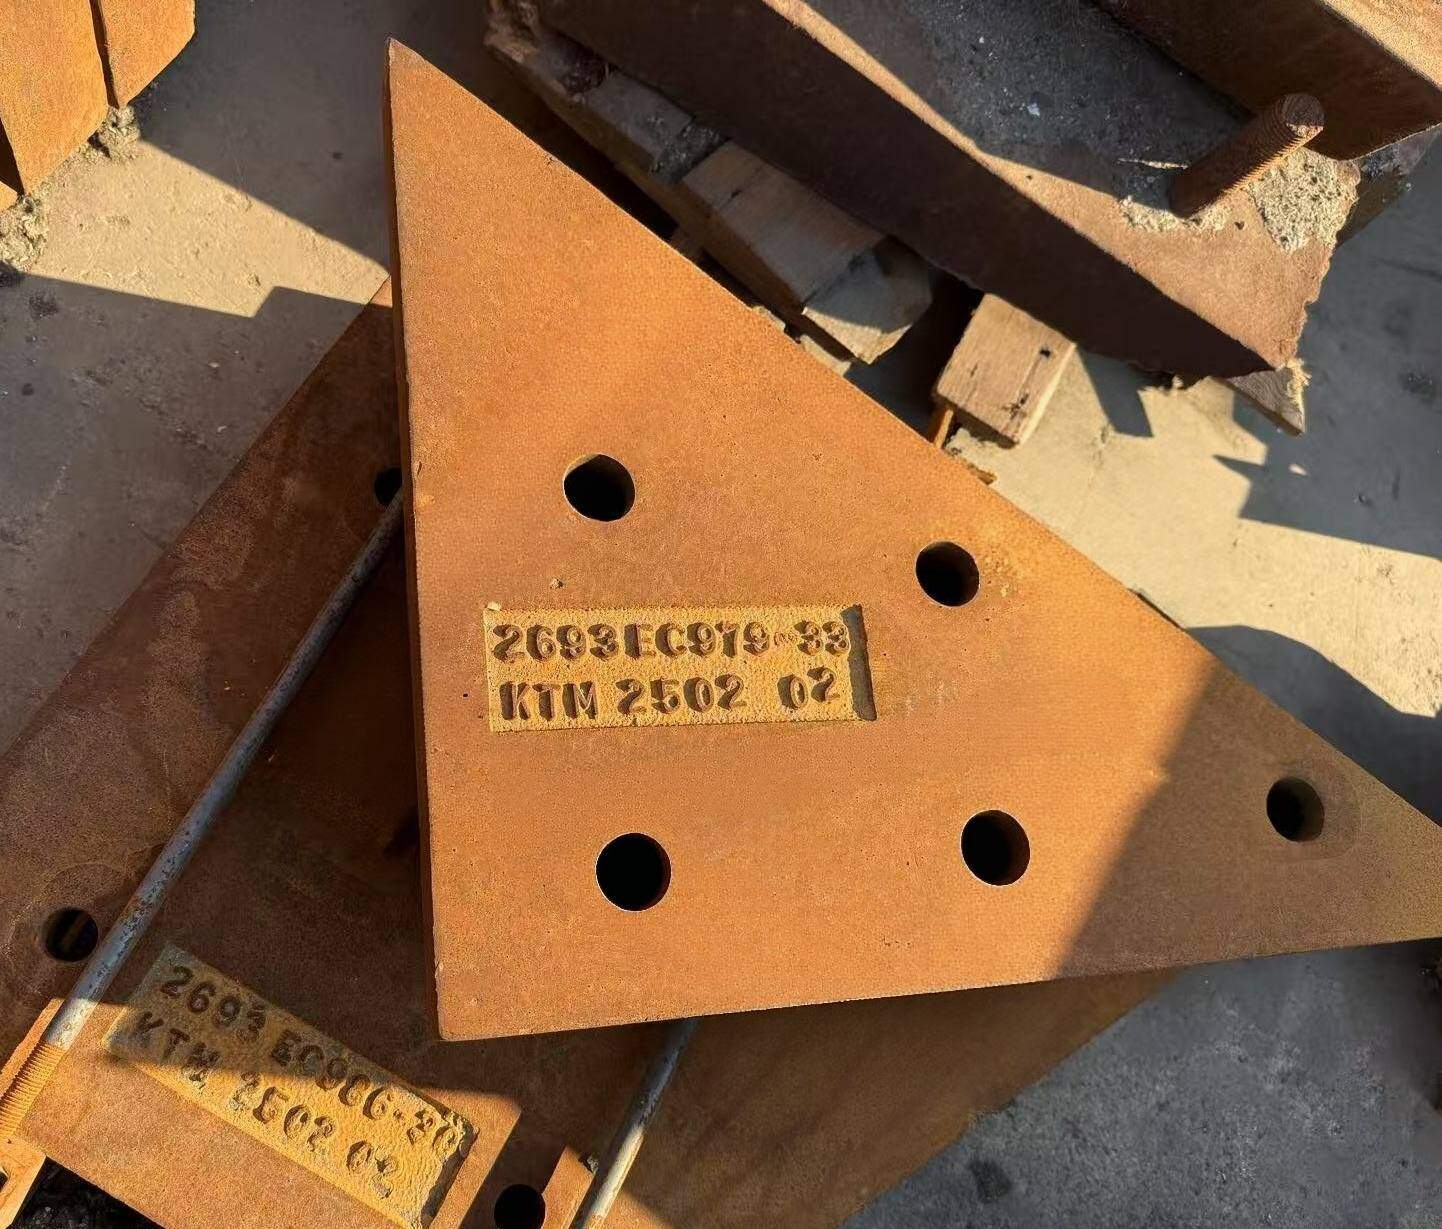
Unique traceability code
Each casting is assigned a unique traceability code that links it to its complete production and inspection records.
26-0417-A
- MARTENSITIC CAST STEEL
- HAMMER / OEM SPEC
- QT-1050 / 2H
- MPI + UT PASSED
- HRC 47.5
Each casting is assigned a unique traceability code that links it to its complete production records.
In-House NDT and Mechanical Testing
We carry out the common non-destructive and mechanical tests on site, so results are available with the parts rather than after a third-party queue.
Magnetic Particle Inspection
Surface and near-surface crack detection
Ultrasonic Testing
Internal discontinuity detection
X-Ray Radiography
Internal shrinkage and porosity evaluation
Dye Penetrant Testing
Surface defect detection on finished faces
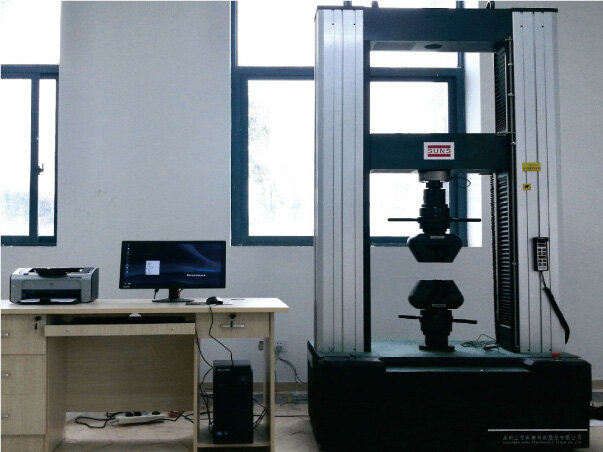
Tensile Testing
Yield and tensile strength verification
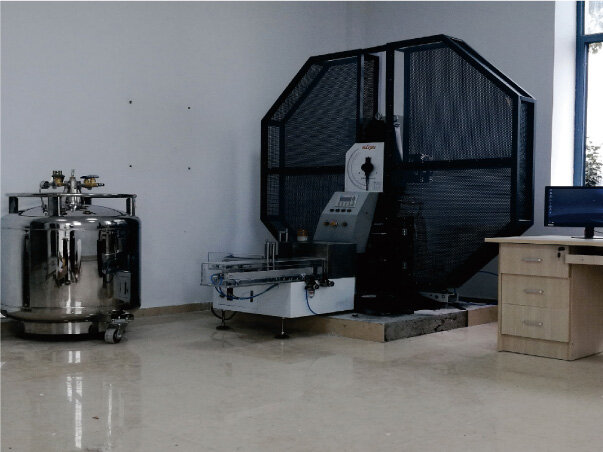
Impact Testing
Toughness verification at specified temperature
Hardness Testing
Hardness verification against the target range
Metallographic Analysis
Microstructure and heat treatment verification
Need inspection records with your order?
Tell us which tests your specification requires and we will confirm the inspection plan before production.